

Maximum Allowable Carryover (MACO) in Cleaning Validation
Maximum Allowable Carryover (MACO) defines the maximum quantity of residue from a previously manufactured product that may theoretically carry into a subsequently manufactured product without causing the patient receiving the subsequent product to exceed the established health-based exposure limit for the previous product.
MACO therefore connects toxicological risk with manufacturing reality. The Health-Based Exposure Limits for Cleaning Validation assessment establishes an acceptable daily exposure such as a PDE or ADE. The MACO calculation then considers how much of the subsequent product a patient may consume and how much subsequent product is manufactured in the smallest applicable batch. The resulting mass of allowable carryover can then be allocated across the shared product-contact equipment and converted into surface, swab, or rinse acceptance criteria.
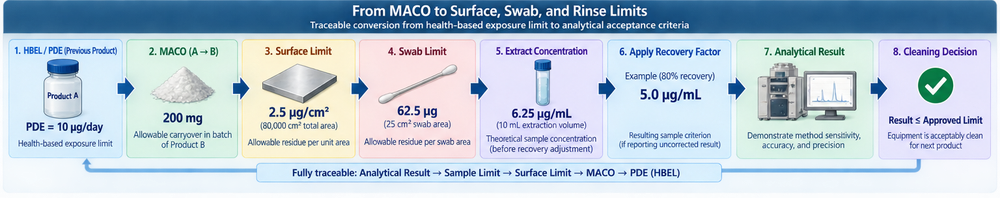
The calculation chain should remain traceable: HBEL / PDE / ADE → MACO → shared equipment allocation → surface limit → swab or rinse criterion → analytical result → cleaning decision
MACO is therefore not an analytical detection limit and is not itself normally the value compared directly with a laboratory result. It is an intermediate patient-safety-based quantity used to derive measurable cleaning-validation acceptance limits.
Regulatory and Scientific Basis
21 CFR 211.67 requires equipment to be cleaned at appropriate intervals to prevent contamination that could alter drug-product safety, identity, strength, quality, or purity. It also requires written procedures describing cleaning methods and materials.
FDA’s Guide to Inspections: Validation of Cleaning Processes does not prescribe a universal MACO formula. Instead, FDA states that the manufacturer’s rationale for residue limits should be logical based on knowledge of the materials involved and that limits should be practical, achievable, and verifiable. FDA expects predefined acceptance criteria, suitable sampling methods, sufficiently sensitive analytical procedures, and documented evidence that residues have been reduced to an acceptable level.
FDA’s ICH Q7 guidance similarly states that cleaning-validation residue limits should consider potency, toxicity, stability, solubility, and difficulty of cleaning. The guidance requires acceptable cleaning levels to be defined and justified and expects cleaning validation to reflect actual equipment-use patterns.
The EMA HBEL guideline provides the most explicit regulatory framework for deriving toxicological threshold values such as PDE and states that these values can be used to justify carryover limits for cleaning validation. EMA’s subsequent Q&A also cautions that the calculated HBEL should not automatically be treated as the routine cleaning-process limit; operational cleaning limits can appropriately remain below the health-based boundary.
MACO Is Not the Same as the HBEL
The HBEL and MACO answer different questions.
The HBEL, PDE, or ADE answers: How much of Product A can a patient be exposed to per day without an appreciable health risk?
The MACO answers: Given that exposure limit, how much Product A could theoretically be distributed through a batch of Product B without causing a patient taking the maximum daily amount of Product B to exceed the Product A HBEL?
This distinction matters because the HBEL is generally expressed as mass per patient per day, such as µg/day or mg/day, whereas MACO is expressed as a total mass of the previous product permitted in the subsequent batch, such as µg or mg.
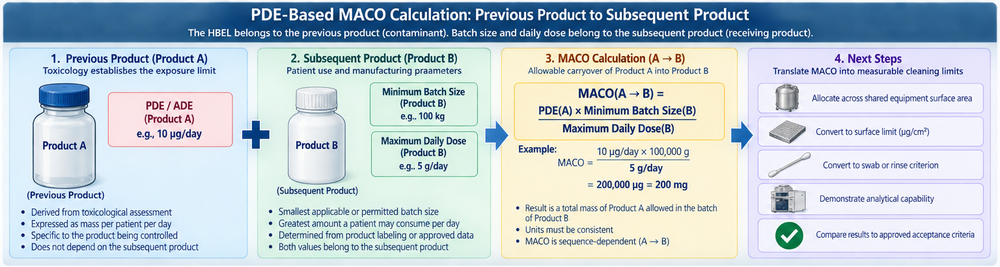
The HBEL belongs to the previous product, because that is the contaminant. The batch size and maximum daily dose belong to the next product, because those parameters determine how much of the contaminated batch a patient could consume.
The PDE-Based MACO Formula
A commonly used health-based MACO relationship is: MACO(A→B) = PDE(A) × Minimum Batch Size(B) ÷ Maximum Daily Dose(B)
Where:
A = previous product, the potential contaminant
B = subsequent product
PDE(A) = PDE or ADE of Product A
Minimum Batch Size(B) = smallest permitted or applicable batch of Product B
Maximum Daily Dose(B) = greatest amount of Product B a patient may consume per day
The result is the allowable mass of Product A that could theoretically be present throughout the applicable batch of Product B while maintaining exposure to Product A at or below its HBEL.
The equation can also be expressed as: MACO = HBELprevious × Batch Sizenext ÷ Maximum Daily Dosenext
The terminology PDE, ADE, or HBEL should remain consistent with the approved toxicological assessment.
Why the Minimum Subsequent Batch Size Is Used
The batch-size term should be understood rather than inserted mechanically. For a fixed amount of previous-product residue, a smaller subsequent batch provides less dilution. Consequently, where batch size enters the approved MACO model in the numerator, the minimum applicable subsequent-product batch size produces the more restrictive carryover limit.
For example, if 100 mg of residue were distributed throughout a 1,000 kg batch, its concentration would be lower than if the same 100 mg were distributed throughout a 100 kg batch. The smaller batch therefore represents the greater potential patient exposure for the same amount of carryover.
This is why describing the “maximum next-product batch size” as automatically conservative is incorrect in a PDE-based MACO calculation.
The batch size should represent an actual permitted manufacturing condition. An artificially small batch that cannot be manufactured should not be introduced simply to produce a more restrictive number unless the calculation procedure specifically requires that assumption.
Why the Maximum Daily Dose of the Subsequent Product Is Used
The maximum daily dose determines how much of the subsequent product a patient could consume in one day. A patient consuming more Product B could also receive more residual Product A.
Therefore, a larger daily dose of Product B produces a lower allowable MACO for Product A.
The dose should normally represent the maximum labeled or otherwise scientifically justified daily quantity of the subsequent product as consumed, using a basis consistent with the batch-size term.
This unit basis deserves particular attention. If the batch size is expressed as kilograms of finished Product B, the daily dose should also represent mass of finished Product B consumed per day, not simply milligrams of Product B’s API per day unless the calculation has been specifically structured on that basis.
For tablets, the calculation can alternatively use: tablets per batch ÷ maximum tablets per patient per day
For a liquid product: liters per batch ÷ maximum liters or milliliters consumed per day
The ratio must describe what fraction of the subsequent batch a patient can consume per day.
Previous Product Versus Subsequent Product
A useful way to prevent calculation errors is to label every MACO calculation explicitly: Product A → Product B rather than simply listing “Product A MACO.”
Consider: Product A → Product B
The required inputs are:
- PDE/ADE of Product A
- minimum batch size of Product B
- maximum daily dose of Product B
Now consider: Product A → Product C
The PDE of Product A remains unchanged, but Product C may have a different minimum batch size and different maximum daily dose. Therefore: MACO(A→B) may not equal MACO(A→C).
This is why a single MACO value assigned permanently to Product A can be misleading in a multiproduct facility.
MACO Is Sequence-Dependent
For facilities manufacturing multiple products on shared equipment, the potential product sequence can materially affect the allowable carryover.
Assume Product A has a PDE of 10 µg/day.
If Product B has:
- minimum batch size = 100 kg
- maximum daily dose = 5 g/day
and Product C has:
- minimum batch size = 50 kg
- maximum daily dose = 10 g/day
the two allowable carryover values are different even though Product A’s toxicology has not changed.
For A → B:
MACO = 10 µg/day × 100,000 g ÷ 5 g/day
MACO = 200,000 µg = 200 mg
For A → C:
MACO = 10 µg/day × 50,000 g ÷ 10 g/day
MACO = 50,000 µg = 50 mg
Product C therefore creates the more restrictive subsequent-product condition.
This is also why Worst-Case Product, Equipment, and Cleaning Condition Selection should consider subsequent-product conditions rather than rank only the product being cleaned.
Unit Consistency Is Critical
Many MACO errors are not toxicological errors. They are unit errors.
All calculations should use a controlled and internally consistent set of units. If the PDE is expressed in µg/day, the resulting MACO will remain in µg provided the batch-size and daily-dose units cancel correctly.
For example: 10 µg/day × 100,000 g ÷ 5 g/day = 200,000 µg
The grams cancel: µg/day × g ÷ g/day = µg
A calculation using:
- batch size in kg;
- daily dose in mg/day;
- PDE in µg/day;
without explicit conversion can produce an error of several orders of magnitude.
A controlled calculation worksheet should display units with every input and intermediate result rather than treat them as labels added after the arithmetic. Typical compatible approaches include:
| Subsequent product basis | Batch-size unit | Daily-dose unit |
|---|---|---|
| Solid formulation by mass | g/batch | g/day |
| Solid formulation by mass | mg/batch | mg/day |
| Tablet/capsule count | units/batch | units/day |
| Liquid product | mL/batch | mL/day |
| Liquid product | L/batch | L/day |
The batch and daily-dose terms must represent the same product basis.
Worked PDE-Based MACO Example
Assume: Previous product: Product A
PDE(A) = 10 µg/day
Subsequent product: Product B
- Minimum batch size(B) = 100 kg
- Maximum daily dose(B) = 5 g/day
First convert the batch size:
100 kg = 100,000 g
Then: MACO(A→B) = 10 µg/day × 100,000 g ÷ 5 g/day
MACO(A→B) = 200,000 µg
MACO(A→B) = 200 mg
The patient-safety-based maximum allowable carryover of Product A into the 100 kg Product B batch is therefore 200 mg, subject to the assumptions and scope of the approved calculation methodology. That 200 mg is not yet a swab acceptance limit. It must first be related to the shared equipment through which Product A residue could transfer into Product B.
Shared Product-Contact Surface Area
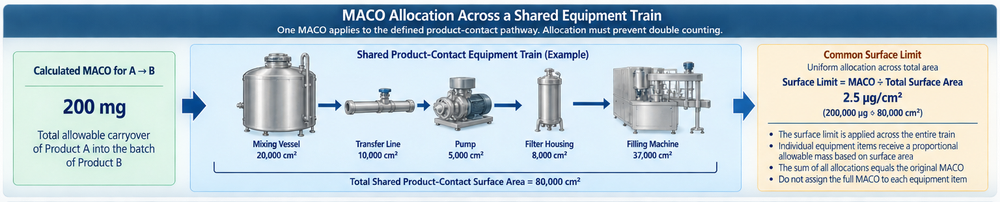
A common approach is to distribute the MACO across the applicable shared product-contact surface area. If the total relevant shared surface area is: 80,000 cm²
then: Surface Limit = MACO ÷ Shared Product-Contact Surface Area
Using the example:
Surface Limit = 200,000 µg ÷ 80,000 cm²
Surface Limit = 2.5 µg/cm²
This means that a uniform theoretical distribution of residue at 2.5 µg/cm² across 80,000 cm² would equal the 200 mg MACO.
The calculation does not mean that residue physically distributes uniformly. Actual cleaning residues tend to concentrate at difficult locations such as gaskets, valves, crevices, transfer connections, spray shadows, or poorly drained surfaces. The surface calculation provides a controlled allocation basis; the sampling strategy must still challenge locations most likely to retain residue.
Defining the Correct Shared Surface Area
The denominator should reflect the actual product-contact pathway relevant to the product sequence. Surface-area assessments should consider:
- vessels;
- agitators;
- internal piping;
- transfer lines;
- pumps;
- valves;
- hoses;
- filters where applicable;
- filling paths;
- removable product-contact components;
- gaskets and other relevant interfaces.
Surfaces used exclusively by the previous product but incapable of transferring residue into the subsequent product may not belong in the same exposure pathway. Conversely, small components should not be omitted simply because their surface area is difficult to calculate if they can retain and transfer residue.
The equipment-train boundary should therefore be consistent with Cleaning Validation Program Strategy, Scope, and Lifecycle and the actual manufacturing flow.
Equipment-Train Allocation
One of the most important MACO controls is ensuring that the total allowable carryover is not inadvertently assigned multiple times.
Suppose the 200 mg MACO applies to an equipment train containing:
- vessel;
- transfer line;
- pump;
- filler.
If every equipment item is independently assigned the full 200 mg MACO, the train could theoretically contain:
200 + 200 + 200 + 200 = 800 mg
while the patient-safety calculation allowed only 200 mg for the entire product pathway. That is incorrect unless a separate scientifically justified exposure model supports it.
A uniform surface limit avoids this problem when it is calculated using the total relevant surface area: Surface Limit = MACO ÷ Total Shared Surface Area
Each equipment component then receives an implied allowable mass proportional to its area, while the sum across the train remains equal to the original MACO. Alternative allocation strategies can be used, but the calculation should demonstrate that the total allocated residue cannot exceed the applicable carryover limit.
Converting the Surface Limit into a Swab Criterion
A surface limit can be converted into an allowable amount associated with a defined swab area.
Using the example:
- Surface limit = 2.5 µg/cm²
- Swabbed area = 25 cm²
Theoretical allowable residue in the sampled area is: 2.5 µg/cm² × 25 cm² = 62.5 µg/swab area
If the swab is extracted in 10 mL: 62.5 µg ÷ 10 mL = 6.25 µg/mL
This is the nominal extract concentration corresponding to a surface exactly at the cleaning limit under complete transfer and with no additional dilution.
Additional sample-preparation factors must then be considered, including:
- swab recovery;
- extraction recovery;
- dilution;
- sample concentration;
- analytical reporting convention.
The relationship between the cleaning limit and the analytical sample is addressed in Analytical Sensitivity and Quantitation Limits in Cleaning Validation.
Treatment of Sampling Recovery
Recovery should be handled according to a predefined site procedure rather than inserted inconsistently into individual MACO calculations.
Assume the theoretical swab-extract criterion is: 6.25 µg/mL and validated recovery is: 80%
A surface containing residue exactly at the theoretical limit might produce approximately: 6.25 × 0.80 = 5.0 µg/mL in the recovered sample, assuming the recovery study represents the actual surface and sampling procedure.
Two common approaches are possible:
- report the analytical result after applying an approved recovery correction; or
- report the uncorrected result and establish the applicable sample criterion accordingly.
Neither approach should be mixed across calculations. Swab and Rinse Recovery Studies for Cleaning Validation should define the recovery convention used by the program.
MACO itself should generally remain a patient-exposure calculation. Sampling recovery affects interpretation of the sample relative to the surface criterion; it does not alter the toxicological HBEL.
Converting MACO into a Rinse Criterion
Where a defined rinse is used to represent the applicable equipment surface, an allowable theoretical concentration can be calculated from the mass allocated to the rinsed system and the applicable rinse volume.
If the full 200 mg MACO applies to an entire equipment train and a validated 50 L rinse quantitatively represents that train:
- Rinse Criterion = 200 mg ÷ 50 L
- Rinse Criterion = 4 mg/L
Since: 1 mg/L = 1 µg/mL the theoretical concentration is: 4 µg/mL
This calculation should not be interpreted as proof that a rinse sample provides the same information as direct surface sampling. Rinse sampling can dilute localized contamination and depends on rinse distribution, accessibility, solubility, volume, and recovery. These limitations are addressed in Rinse Sampling for Cleaning Validation.
Surface Limits, Swab Limits, and Rinse Limits Must Remain Traceable
A robust cleaning-validation calculation should allow movement in both directions.
Forward: PDE → MACO → surface limit → sample criterion and backward: Analytical result → sample criterion → surface limit → MACO → PDE
This traceability makes it possible to determine whether a reported laboratory result truly supports the patient-safety basis of the cleaning acceptance criterion. It also makes changes easier to assess. If a PDE changes, the impact on downstream MACO, surface, swab, rinse, and analytical limits can be recalculated systematically.
Multiple Products Require a Carryover Matrix
A multiproduct facility should not assume that one MACO per previous product is sufficient.
A product-to-product matrix can evaluate the relevant manufacturing sequences:
| Previous product | Next product | PDE previous | Minimum batch next | Maximum daily dose next | Calculated MACO |
|---|---|---|---|---|---|
| A | B | Input A | Input B | Input B | A→B |
| A | C | Input A | Input C | Input C | A→C |
| B | A | Input B | Input A | Input A | B→A |
| B | C | Input B | Input C | Input C | B→C |
The lowest applicable MACO may then be selected as a conservative limit for a shared cleaning group, provided the grouping remains scientifically justified.
This approach can simplify routine operations because the cleaning procedure does not need a different residue criterion for every possible product sequence. However, the conservative group limit should still be achievable by the cleaning process and measurable by the analytical method.
A matrix also makes clear when a newly introduced product creates a more restrictive sequence than those previously validated.
MACO and Worst-Case Selection
The lowest MACO can identify a toxicological or exposure-based worst case, but it should not be treated as the only cleaning worst-case criterion. Another product may be substantially more difficult to remove because of:
- poor cleanability;
- hydrophobic formulation;
- polymers or oils;
- residue aging;
- long dirty hold time;
- equipment interaction;
- difficult analytical detection.
Therefore Worst-Case Product, Equipment, and Cleaning Condition Selection should consider MACO alongside cleanability, formulation, equipment design, surface materials, campaign conditions, dirty hold, and analytical capability.
A product can represent the lowest allowable carryover without representing the most difficult cleaning challenge.
Historical Dose-Based and 10-ppm Criteria
Cleaning-validation programs historically used criteria such as:
- a fraction of the minimum therapeutic dose of the previous product;
- a 10-ppm carryover criterion;
- visually clean equipment.
These approaches played an important role before widespread use of compound-specific toxicological exposure limits. They should not be confused with a PDE-based MACO calculation.
A PDE-based calculation uses: PDE of the previous product and: minimum batch size and maximum daily dose of the subsequent product
A traditional dose-based formula may use the therapeutic dose of the previous product and an additional safety factor. Mixing variables from these two calculation approaches creates a scientifically incoherent hybrid.
Where an organization retains a historical limit that is more restrictive than the HBEL-based limit, it may be maintained as an operational or alert limit when scientifically and procedurally justified. EMA’s HBEL Q&A explicitly recognizes this concept rather than requiring every cleaning process to operate exactly at the calculated HBEL boundary.
Avoid Arbitrary Additional Safety Factors
A properly derived PDE or ADE already contains toxicological adjustment factors addressing uncertainty in the underlying evidence. The Health-Based Exposure Limits for Cleaning Validation article explains how factors such as species extrapolation, human variability, study duration, serious toxicity, and absence of an appropriate NOAEL can be incorporated into the toxicological assessment.
Automatically applying another arbitrary factor such as 1/10 or 1/100 to the resulting PDE-based MACO may duplicate conservatism without a defined scientific basis.
An organization can intentionally establish an operational cleaning limit below the patient-safety boundary. That can provide process-control margin and may be entirely appropriate. The distinction should simply remain clear:
- HBEL-derived limit = health-based boundary
- Operational target or alert limit = process-control decision
The latter should not be represented as an additional regulatory toxicological factor unless such a factor has actually been justified.
Detergent and Cleaning-Agent Limits
The PDE-based product MACO formula should not automatically be applied to detergents, sanitizers, solvents, or other cleaning agents.
Cleaning-agent residues require their own scientifically justified acceptance basis. Depending on the material, this may involve toxicological information, permitted exposure, supplier data, concentration in the cleaning formulation, rinse capability, TOC, conductivity, or chemical-specific analysis.
A product-residue MACO demonstrates control of carryover from the previous manufacturing product. It does not demonstrate that cleaning chemicals have been adequately removed.
Cleaning Validation Acceptance Criteria and Surface, Swab, and Rinse Limits should integrate the applicable product, cleaning-agent, visual, and other residue criteria.
Analytical Capability Must Be Evaluated After the Limit Is Calculated
The acceptance limit should drive the analytical requirement, not the reverse.
After the surface or sample criterion has been calculated, Analytical Method Selection for Cleaning Validation should identify an appropriate measurement technology. Analytical Sensitivity and Quantitation Limits in Cleaning Validation should then confirm that the required concentration lies within practical quantitative capability, while Analytical Method Validation for Cleaning Residue Testing should demonstrate appropriate accuracy, precision, specificity or selectivity, range, recovery, matrix control, and robustness.
If the calculated criterion cannot be measured reliably, the response should be to evaluate:
- a more capable analytical procedure;
- different sample preparation;
- larger swab area;
- smaller extraction volume;
- alternative sampling;
- justified nonspecific testing;
- improved cleaning;
- additional segregation or containment;
- dedicated product-contact components.
The HBEL or MACO should not be increased simply because the existing analytical procedure cannot measure the resulting criterion.
Significant Figures and Rounding
Cleaning limits should not imply greater precision than the source data support.
A PDE may contain uncertainty inherent in toxicological data, while equipment surface areas, batch sizes, recovery factors, and analytical measurements each introduce additional variability. Reporting a surface criterion such as: 2.483716 µg/cm² is generally misleading when the underlying inputs do not justify that precision.
Calculation procedures should define:
- number of significant figures retained during intermediate calculations;
- final rounding convention;
- whether final values are rounded conservatively;
- units used in master data and protocols.
Intermediate values should generally retain adequate precision so repeated rounding does not materially alter the final result.
Calculation Verification and Data Integrity
MACO worksheets can become complex when a facility has many products, equipment trains, dose strengths, batch sizes, and cleaning groups. The calculation system should therefore be controlled with the same discipline applied to other GMP calculations.
Controls should include:
- approved source for each PDE/ADE;
- approved batch-size information;
- approved maximum daily dose;
- controlled equipment surface areas;
- explicit units;
- verified formulas;
- independent calculation review;
- version control;
- change history;
- protection against unintended formula changes.
Where spreadsheets are used, formula logic, input cells, calculations, access, change control, and verification should be appropriate to the GMP risk of the application.
A calculation is not adequately controlled merely because another person confirms that the final number “looks reasonable.”
Calculation Documentation
Each MACO assessment should identify the assumptions and data sources sufficiently for another reviewer to reconstruct the calculation.
At minimum, document:
- previous product;
- subsequent product;
- approved PDE/ADE/HBEL source;
- applicable minimum subsequent batch size;
- applicable maximum subsequent daily dose;
- units and conversions;
- MACO equation;
- calculated MACO;
- equipment train;
- shared product-contact surface area;
- allocation methodology;
- calculated surface limit;
- swab area and extraction volume where applicable;
- rinse volume where applicable;
- recovery convention;
- analytical criterion;
- calculation author and verifier;
- approval date and revision.
Where one conservative MACO is selected to represent several product sequences, the calculation should identify the underlying matrix and demonstrate why the selected value covers the intended scope.
Change Control
MACO calculations should be reassessed when an input or assumption changes. Potential triggers include:
- revised PDE or ADE;
- new product;
- new product strength;
- revised maximum daily dose;
- new minimum batch size;
- new equipment train;
- changed product-contact surface area;
- equipment modification;
- changed product sequence;
- new cleaning group;
- revised recovery strategy;
- changed analytical method.
A change in PDE can propagate through every downstream limit: PDE → MACO → surface criterion → sample criterion → analytical capability
The impact assessment should determine whether existing cleaning-validation data remain acceptable against the revised limit.
Cleaning Validation Change Control and Revalidation Triggers should govern whether recalculation alone is sufficient or whether targeted verification or revalidation is required.
Periodic Review
Periodic review should verify that the master data supporting MACO calculations remain current.
The review should consider product portfolio changes, toxicological updates, batch-size changes, labeling changes affecting maximum daily dose, equipment modifications, revised surface areas, analytical changes, and introduction of new product sequences.
Cleaning Validation Periodic Review and Continued Verification should also evaluate whether routine cleaning results remain comfortably within the established limits and whether recurring excursions indicate deterioration of process capability even when the patient-safety MACO has not been exceeded.
Common MACO Calculation Errors
The most consequential MACO errors are usually conceptual rather than mathematical.
Common errors include using the PDE of the next product instead of the previous product; using the batch size of the previous product; using minimum therapeutic dose of the previous product in a PDE-based formula; using maximum rather than minimum applicable subsequent batch size; using minimum rather than maximum subsequent daily dose; and mixing mass, volume, or dosage-unit bases without conversion.
Other common errors include dividing MACO independently across equipment components so that each component receives the full allowable carryover; omitting shared hoses, valves, filters, gaskets, or transfer lines from surface area; treating uniform surface allocation as proof that residues are actually uniformly distributed; applying recovery inconsistently; and confusing the laboratory LOQ with the patient-safety acceptance limit.
Calculation governance problems include obsolete PDE values, outdated product labels, incorrect surface-area drawings, uncontrolled spreadsheets, hard-coded conversion factors, excessive decimal precision, and failure to reassess calculations when new products are introduced.
Worked Example Summary
Using the example developed above:
| Parameter | Value |
|---|---|
| Previous product PDE | 10 µg/day |
| Subsequent minimum batch size | 100 kg = 100,000 g |
| Subsequent maximum daily dose | 5 g/day |
| Calculated MACO | 200 mg |
| Shared surface area | 80,000 cm² |
| Surface criterion | 2.5 µg/cm² |
| Swab area | 25 cm² |
| Residue corresponding to one swab area | 62.5 µg |
| Extraction volume | 10 mL |
| Nominal extract criterion before recovery treatment | 6.25 µg/mL |
The calculation chain is: 10 µg/day × 100,000 g ÷ 5 g/day = 200,000 µg = 200 mg
then: 200,000 µg ÷ 80,000 cm² = 2.5 µg/cm²
then: 2.5 µg/cm² × 25 cm² = 62.5 µg/swab area
then: 62.5 µg ÷ 10 mL = 6.25 µg/mL
Each step should be documented separately so changes can be evaluated without reconstructing the calculation from an unexplained final number.
Key Principles
- MACO translates an allowable daily exposure to a previous-product residue into the maximum total amount that may carry into a subsequent product under a defined manufacturing scenario.
- In a PDE-based calculation, the PDE or ADE belongs to the previous product, while minimum batch size and maximum daily dose belong to the subsequent product. Product sequence therefore matters, and one previous product can have different MACO values depending on what is manufactured next.
- The minimum applicable subsequent batch size and maximum applicable subsequent daily dose normally produce the more restrictive values in the standard PDE-based MACO relationship.
- Units should remain explicit and consistent throughout the calculation. Batch size and daily dose must use the same product basis so that their units cancel correctly.
- MACO should be allocated across the actual shared product-contact pathway without double counting. Dividing the MACO by total relevant shared surface area provides one practical method of establishing a common surface criterion, but the sampling strategy must still target locations most likely to retain residue.
- Surface limits must then be translated into swab, rinse, or other sample-specific acceptance criteria. Sampling recovery and analytical capability should be handled according to controlled procedures rather than altering the toxicological basis of the MACO.
- The PDE-based equation is a scientifically established industry approach, not a numerical formula explicitly mandated by FDA. FDA’s regulatory expectation is that residue limits be justified, appropriate for the products and equipment, and supported by suitable sampling and analytical evidence.
- MACO calculations should remain under lifecycle control. Revised HBELs, product doses, batch sizes, equipment surface areas, product sequences, and analytical methods should trigger documented assessment of the existing cleaning limits and validation evidence.