

Rinse Sampling for Cleaning Validation
Rinse sampling is an indirect cleaning-validation method used to evaluate residues from equipment surfaces that cannot be sampled adequately by direct surface methods. It is particularly useful for closed piping, transfer lines, hoses, vessels with restricted access, filters, complex flow paths, and other product-contact surfaces where representative swabbing is impractical.
The principal advantage of rinse sampling is coverage. A properly designed rinse can contact a much larger product-contact area than a localized swab and can provide evidence from surfaces that cannot be reached physically. Its principal limitation is the same characteristic: the analytical result represents residue recovered into a bulk liquid volume and therefore provides an averaged system-level measurement rather than direct evidence from a specific surface location.
A low rinse result does not necessarily demonstrate that every product-contact location is below the corresponding surface residue limit. Localized residue trapped in a valve, gasket interface, low point, dead-ended section, spray shadow, or poorly contacted surface can be diluted by a large rinse volume or may not be recovered at all.
For that reason, FDA states that rinse sampling alone is generally not sufficient for cleaning validation when direct measurement of accessible equipment surfaces is feasible. FDA recognizes combined swab and rinse strategies when the rinse solvent has been demonstrated to dissolve the residues of concern and is otherwise appropriate for the sampled surfaces.
Role of Rinse Sampling in the Cleaning Validation Strategy
Rinse sampling should be selected because it provides meaningful evidence for defined equipment surfaces, not simply because collecting a liquid sample is easier than swabbing equipment.
Cleaning Validation Sampling Strategy and Worst-Case Locations should first map the equipment and classify product-contact surfaces according to accessibility, residue-retention risk, geometry, drainage, cleaning mechanism, and available sampling methods. Rinse sampling is then applied where indirect measurement provides the most appropriate or practical evidence.
Typical applications include:
- internal transfer piping;
- flexible product hoses;
- manifolds;
- narrow tubing;
- filter housings;
- inaccessible vessel surfaces;
- complex closed systems;
- equipment that cannot be routinely disassembled;
- systems handling hazardous materials where direct access creates unacceptable exposure risk.
ICH Q7 specifically recognizes that direct swabbing may be impractical for the internal surfaces of hoses, transfer pipes, vessels with small ports, and small intricate equipment. It permits swabbing, rinsing, or alternative approaches as appropriate, while requiring the sampling method to quantitatively measure residues remaining after cleaning.
Rinse Sampling Is an Indirect Measurement
A rinse result measures the material recovered into a defined liquid. It does not directly measure residue remaining on the equipment surface.
The measurement chain is therefore:
Residue on equipment → contact with rinse liquid → dissolution or physical removal → transport through the equipment → collection of representative rinse → analytical measurement → recovery interpretation → comparison with acceptance criterion
Each step can influence the result.
A low laboratory concentration can result from effective cleaning, but it can also result from poor residue solubility, incomplete surface contact, excessive rinse volume, incomplete collection, residue remaining trapped in the system, adsorption to equipment, or inadequate analytical sensitivity.
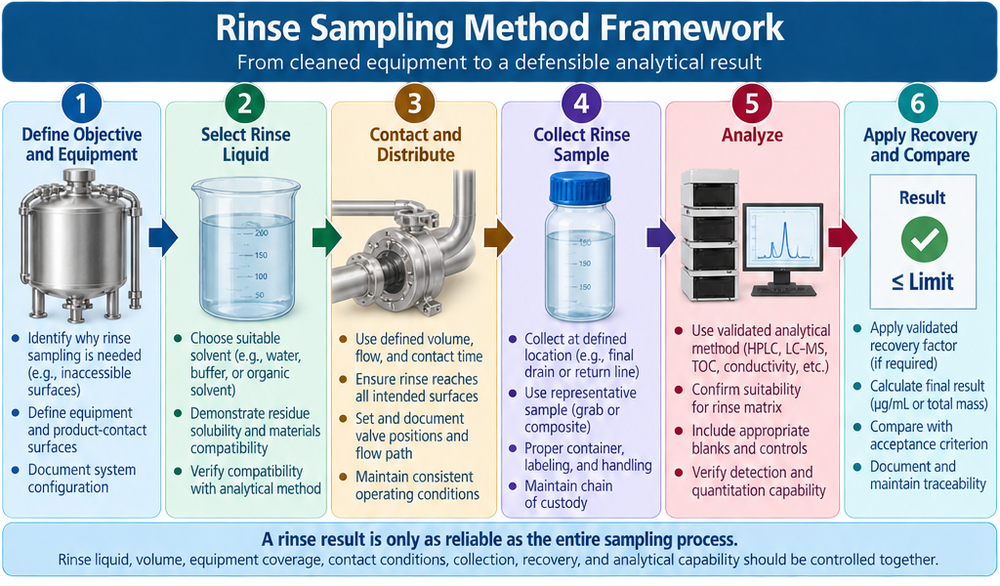
Rinse sampling should therefore be treated as a sampling and extraction procedure, not merely as collecting water from the end of a cleaning cycle.
Final Process Rinse and Dedicated Analytical Rinse Are Different
A cleaning-validation program should distinguish between a final process rinse and a dedicated analytical rinse. They can both provide useful evidence, but they represent different sampling concepts.
A final process rinse is the liquid generated as part of the approved cleaning procedure. For example, the validated CIP cycle may conclude with a purified-water rinse that is collected or sampled for residue analysis.
A dedicated analytical rinse is a separate, controlled rinse performed specifically to recover residual material from the cleaned equipment for analytical evaluation. It occurs after the cleaning procedure and is designed as a sampling operation rather than as a cleaning step.
The distinction should be explicit because the rinse liquid, volume, contact conditions, and interpretation may be different.
Final Process Rinse Sampling
Sampling the final routine cleaning rinse has an important advantage: it evaluates the actual process output. The result can provide direct evidence of what remains in the liquid leaving the equipment at the defined endpoint of cleaning.
A final process rinse may be particularly useful when the cleaning procedure includes controlled parameters such as:
- fixed final-rinse volume;
- conductivity endpoint;
- TOC endpoint;
- defined recirculation period;
- fixed number of rinse cycles;
- defined water quality;
- controlled flow or pressure.
However, the sample should still be evaluated for the residue of concern or a scientifically justified surrogate. Demonstrating only that final rinse water meets its incoming purified-water or WFI chemical specification does not demonstrate adequate removal of the previous product.
FDA’s cleaning-validation inspection guide specifically distinguishes residue testing of the rinse from generic water-quality testing. The purpose is to determine whether contaminants remain, not simply whether the water meets a compendial water specification.
Dedicated Analytical Rinse Sampling
A dedicated analytical rinse can be useful where the routine final rinse does not provide adequate residue recovery or where a more controlled extraction condition is needed to evaluate the cleaned equipment.
The dedicated rinse procedure should define:
- rinse solvent;
- rinse volume;
- system configuration;
- contact time;
- flow or circulation;
- temperature where relevant;
- agitation where applicable;
- collection method;
- sample location;
- recovery basis;
- analytical method.
Because the dedicated rinse occurs after the cleaning procedure, it should remain clearly identified as a sampling operation. It should not become an undocumented additional cleaning step used to improve cleaning-validation results.
The dedicated rinse should also not be so aggressive that it creates an extraction condition unrelated to the validation objective. The method should provide reliable recovery of relevant residual contamination while remaining scientifically interpretable as a verification technique.
Dedicated Analytical Rinse Is a Sampling Step, Not a Cleaning Step
A dedicated analytical rinse is performed after the approved cleaning procedure has been completed. Its purpose is to recover any residue remaining on the cleaned equipment so that the residue can be measured analytically. Although the rinse may physically remove some residual material during sampling, that is expected because the rinse functions as an extraction method.
The important distinction is whether the rinse is part of the validated cleaning process or part of the sampling procedure.
Approved cleaning procedure → defined cleaning endpoint → dedicated analytical rinse → sample analysis
In this sequence, the analytical rinse does not improve or complete the cleaning process. It simply extracts residue remaining after cleaning so that cleaning effectiveness can be evaluated. By contrast, the following practice is not acceptable as an analytical-rinse strategy:
Cleaning procedure → additional rinse(s) used to further clean the equipment → analytical sampling
If additional rinsing is necessary to achieve acceptable cleanliness, those rinse steps are part of the cleaning process and should be formally defined, controlled, and validated as such.
The analytical-rinse procedure should therefore specify a fixed rinse volume, solvent, contact condition, flow path, and collection method. Repeated rinsing should not be performed simply to obtain a lower analytical result.
Selection of Rinse Solvent
The rinse liquid should be capable of recovering the residue being evaluated from the equipment surfaces.
FDA specifically states that combined rinse and swab sampling is acceptable when the rinse solvent has been demonstrated to dissolve the residues of concern and is suitable for the sampled surfaces. Water may be appropriate for water-soluble product residues, salts, detergents, or other readily soluble materials. Other residues may require a different medium.
Potential rinse liquids can include:
- purified water;
- WFI;
- buffered solutions;
- aqueous mixtures;
- organic or mixed solvents;
- other scientifically justified extraction media.
Selection should consider:
- residue solubility;
- equipment-material compatibility;
- residue stability;
- analytical compatibility;
- operator safety;
- ability to circulate or distribute through the equipment;
- ability to collect the rinse quantitatively or reproducibly.
A rinse solvent should not be selected solely because it is convenient.
Solubility Is Necessary but Not Sufficient
A residue can be soluble in the rinse medium yet still be poorly represented by the rinse sample. Other mechanisms can prevent adequate recovery:
- residue trapped in crevices;
- material shielded from rinse flow;
- adsorption to product-contact materials;
- insufficient contact time;
- poor hydraulic coverage;
- stagnant zones;
- incomplete drainage;
- insufficient mechanical action.
The rinse-recovery study should therefore evaluate the complete rinse procedure, not merely laboratory solubility of the residue in the selected liquid.
Rinse Volume
Rinse volume directly affects the measured concentration.
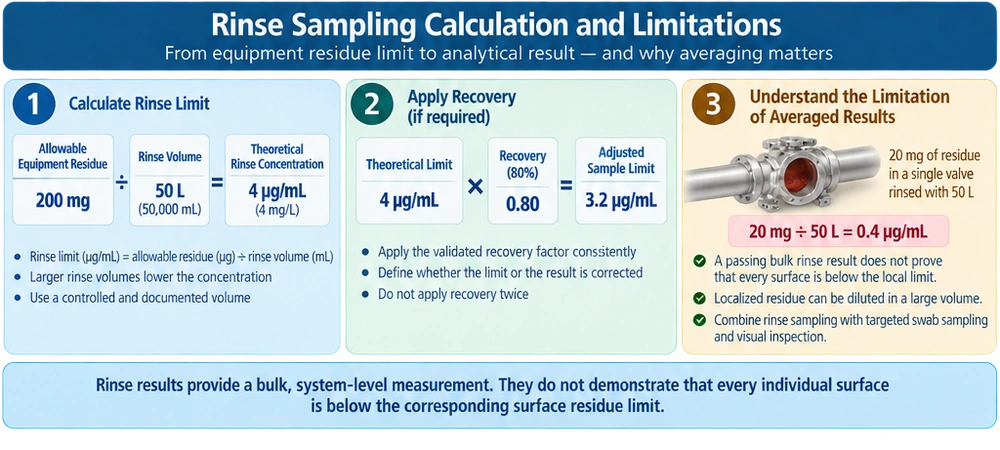
Assume the maximum allowable residue assigned to a rinsed system is: 200 mg
If the analytical rinse volume is: 50 L the theoretical concentration corresponding to the allowable mass is:
- Rinse Limit = 200 mg ÷ 50 L
- Rinse Limit = 4 mg/L = 4 µg/mL
If the same allowable mass were dispersed into 100 L, the concentration would become: 200 mg ÷ 100 L = 2 mg/L = 2 µg/mL
The equipment residue limit has not changed. Only the analytical concentration has changed because the dilution volume changed. Rinse volume should therefore be controlled or accurately documented whenever the result is interpreted quantitatively.
Larger Rinse Volumes Are Not Automatically Better
A larger volume can improve equipment coverage, but it also increases dilution.
Excessive rinse volume can reduce the concentration of residue presented to the analytical method and can make a localized contamination problem more difficult to detect.
The rinse volume should balance:
- adequate surface contact;
- hydraulic distribution;
- residue recovery;
- practical collection;
- analytical sensitivity;
- equipment configuration.
The volume should be established through sampling-method development rather than chosen simply to maximize flushing.
Contact Time
The rinse liquid requires sufficient contact with the surfaces from which residue is intended to be recovered.
Contact can involve:
- filling;
- soaking;
- recirculation;
- dynamic flow;
- spraying;
- agitation;
- repeated controlled passes.
The method should define the relevant contact condition.
A one-minute pass through a complex piping system may not provide the same recovery as a ten-minute controlled recirculation. Conversely, an excessively long extraction may recover material that is physically embedded or otherwise unlikely to transfer under realistic manufacturing conditions.
The contact condition should support the intended sampling objective.
Distribution and Surface Coverage
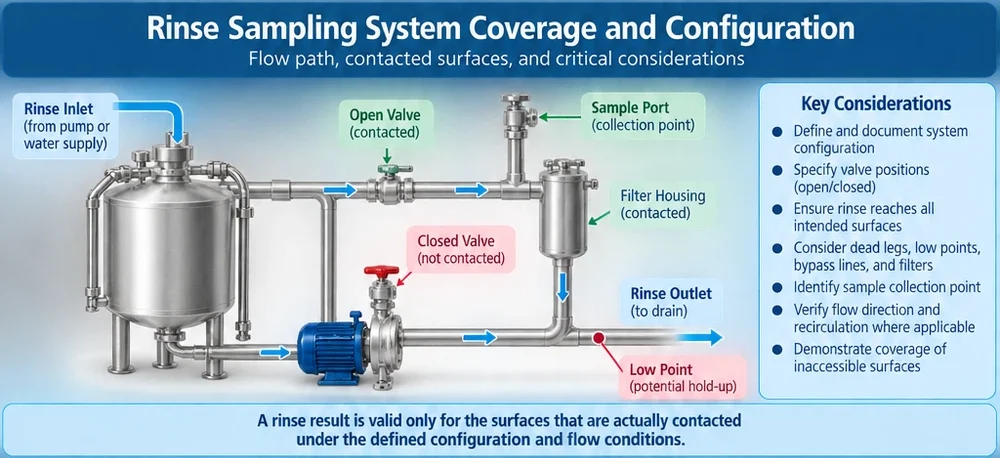
A rinse sample is meaningful only if the rinse liquid reaches the surfaces the result is claimed to represent.
The sampling procedure should therefore consider:
- flow direction;
- valve position;
- system route;
- pump operation;
- spray-device operation;
- bypass lines;
- dead legs;
- filter configuration;
- hose orientation;
- equipment tilt or drainage;
- trapped gas;
- system low points.
If a rinse bypasses an internal valve cavity, that valve cannot reasonably be represented by the rinse result.
Similarly, a rinse collected from one piping branch should not automatically be used to represent another branch that was not exposed to the same rinse conditions.
System Configuration Must Be Defined
Rinse sampling should occur in a defined and reproducible equipment configuration.
The procedure should specify as applicable:
- valves open or closed;
- hoses connected or disconnected;
- filters installed or removed;
- pumps operating or static;
- vessel orientation;
- spray devices active or inactive;
- drain position;
- recirculation route;
- sampling collection point.
A change in configuration can materially change which surfaces are contacted and how residue is recovered.
The validation report should therefore document the configuration represented by the rinse sample.
Inaccessible Surfaces
Rinse sampling is particularly valuable for surfaces that cannot be sampled directly.
Examples include:
- pipe interiors;
- hose interiors;
- small-bore tubing;
- closed transfer systems;
- internal pump pathways;
- filter housings;
- narrow vessel openings.
ICH Q7 specifically recognizes rinse sampling as appropriate where equipment configuration makes swabbing impractical.
The fact that a location is inaccessible, however, does not eliminate the need to understand whether the rinse actually contacts it.
Design knowledge, flow studies, equipment qualification, cleaning-development evidence, or other engineering information may be required to demonstrate that an inaccessible section is represented adequately.
Rinse Sampling and Equipment Design
Poor rinse recovery can expose an underlying equipment-design or cleaning-design problem.
If a product-contact area cannot be:
- directly inspected;
- swabbed;
- contacted adequately by cleaning;
- contacted adequately by a validation rinse;
- otherwise verified;
the issue may not be solvable merely by selecting another analytical method. Equipment design, disassembly, cleaning procedure, sampling access, or product-contact configuration may need to be reconsidered.
A validation strategy should not use indirect sampling to conceal poorly cleanable or unverifiable equipment.
Rinse Concentration Versus Total Rinse Mass
Rinse results can be interpreted as concentration or converted to total recovered mass.
Assume: Measured concentration = 1.5 µg/mL
Rinse volume: 50 L = 50,000 mL
The recovered mass is:
- 1.5 µg/mL × 50,000 mL = 75,000 µg
- 75,000 µg = 75 mg
If the allowable mass assigned to the system is 200 mg, the measured recovered rinse mass is below that allocation.
This conversion can help maintain traceability between the rinse result and the underlying equipment-residue allowance. However, the calculation still represents recovered residue, not necessarily all residue physically present on the equipment unless recovery has been demonstrated adequately.
Rinse Recovery
Rinse recovery describes the efficiency with which the defined rinse procedure removes and collects residue from the surfaces it is intended to represent.
Conceptually: Recovery (%) = Recovered Amount ÷ Known Applied Amount × 100
A recovery study may apply a known quantity of residue to representative surfaces or equipment, allow it to dry or equilibrate under defined conditions, perform the proposed rinse procedure, and measure the amount recovered.
The study should consider:
- relevant surface materials;
- residue concentration;
- residue aging;
- rinse liquid;
- rinse volume;
- contact conditions;
- flow;
- equipment geometry;
- collection efficiency;
- analytical method.
ICH Q7 states that the attainable recovery level of the analytical and sampling method should be established. FDA similarly expects sampling and analytical methods to be challenged together so the degree of recovery is understood.
Recovery on Coupons Versus Actual Equipment
Coupon studies can provide useful information on rinse-liquid extraction from representative materials, but they do not reproduce hydraulic effects within actual equipment.
Full-scale rinse performance can also depend on:
- flow distribution;
- spray coverage;
- turbulence;
- drainage;
- piping orientation;
- valve geometry;
- fluid hold-up.
Where these factors are significant, equipment-level or representative-system studies may be necessary to support the rinse method.
Recovery Correction
As with swab sampling, the site should define how rinse recovery is incorporated into acceptance decisions.
Assume:
- theoretical rinse criterion = 4 µg/mL
- validated recovery = 80%
If results are reported without correction, the expected measured concentration from equipment containing residue exactly at the theoretical limit could be: 4 µg/mL × 0.80 = 3.2 µg/mL
Alternatively, a measured result may be corrected: Corrected Result = Measured Result ÷ Recovery Fraction
The acceptance criterion and reported result should use the same convention. Recovery should not be applied twice.
Cleaning Validation Acceptance Criteria and Residue Limits should establish the program-level convention for recovery treatment.
Averaging Is the Fundamental Limitation of Rinse Sampling
The most important limitation of rinse sampling is dilution of localized residue into a larger volume.
Assume that one small valve contains 20 mg of residue while the remainder of a large equipment train is essentially clean.
If the system is rinsed with: 50 L and the entire 20 mg is recovered: 20 mg ÷ 50 L = 0.4 mg/L = 0.4 µg/mL
The analytical result may appear low even though the valve itself contains significant localized contamination. The situation becomes more problematic if only part of the valve residue is recovered.
This is why a passing rinse result cannot automatically establish that every individual surface is below an area-based surface criterion.
Rinse Results Should Not Be Converted Blindly to µg/cm²
A common mistake is to take the measured total rinse residue and divide it by the total equipment surface area to calculate an apparent average µg/cm² result.
Mathematically: Recovered mass ÷ total area = average equivalent residue per area , but this value should not be represented as direct evidence that every surface contains that concentration. It is an average theoretical distribution. Actual residue may be highly nonuniform.
A direct swab result from a worst-case valve or gasket provides different information and should not be replaced by a calculated average derived from the bulk rinse.
Final Rinse Endpoint Versus Validation Acceptance Criterion
A cleaning process can use an operational endpoint such as:
- conductivity;
- pH;
- TOC;
- visual clarity;
- fixed rinse volume.
That endpoint should not automatically be confused with the final cleaning-validation residue acceptance criterion.
For example, CIP may continue rinsing until conductivity approaches incoming-water conductivity. That endpoint can demonstrate removal of ionic cleaning chemistry but may not directly demonstrate that a specific product residue meets its HBEL-derived acceptance criterion.
Process endpoints and validation acceptance criteria can complement each other, but they should remain conceptually distinct.
TOC for Rinse Samples
FDA recognizes TOC as an acceptable approach for cleaning-validation rinse testing when the residue contains organic carbon that can be oxidized adequately under the method conditions. TOC is nonspecific, so detected carbon generally must be attributed conservatively to the target contaminant when used for comparison with the cleaning limit. Background carbon should also be controlled.
TOC rinse sampling should consider:
- rinse-water background;
- detergent carbon;
- product carbon;
- sampling containers;
- environmental contamination;
- oxidation efficiency;
- carbon conversion factor;
- recovery;
- sample holding time.
A low TOC result should not be interpreted as evidence for residues that do not produce an appropriate TOC response.
Conductivity for Rinse Samples
Conductivity can be useful for detecting ionic cleaning agents or for monitoring rinse endpoints. Its use should be based on demonstrated correlation between the residue concentration and conductivity under the applicable water-quality and temperature conditions.
Conductivity may be highly useful for removing alkaline or acidic detergents yet provide little information about a nonionic API. One rinse sample can therefore require different analytical evaluations depending on the residues being controlled.
Compound-Specific Rinse Testing
HPLC, UPLC, ion chromatography, spectroscopic methods, or other compound-specific techniques may be appropriate where the target residue requires selective quantitation. The analytical procedure should be capable of measuring the residue at the concentration produced by the defined rinse volume and recovery.
Analytical Method Selection for Cleaning Validation should determine whether a specific or nonspecific method is appropriate, while Analytical Sensitivity and Quantitation Limits in Cleaning Validation should determine whether the analytical method has sufficient quantitative capability.
Analytical LOQ and Rinse Volume
Because rinse samples can be highly diluted, analytical LOQ can become a major design constraint.
Assume:
- equipment allowance = 10 mg
- rinse volume = 100 L
The theoretical concentration at the limit is: 10 mg ÷ 100 L = 0.1 mg/L = 0.1 µg/mL. If the analytical LOQ is 0.5 µg/mL, the method cannot reliably quantify the rinse criterion.
Possible responses include:
- smaller rinse volume if coverage remains adequate;
- larger sample volume and concentration;
- more sensitive analytical method;
- alternative analytical technology;
- targeted swab sampling;
- different extraction strategy.
The patient-safety limit should not simply be increased to accommodate inadequate analytical capability.
Sample Collection Point
The rinse sample should be collected at a location that represents the intended rinse pathway.
Potential locations include:
- system return;
- final equipment drain;
- dedicated sample port;
- vessel outlet;
- recirculation return.
The collection point should avoid unrepresentative stagnant liquid unless that stagnant location is itself the intended challenge. Where a rinse recirculates before sampling, the procedure should define how sufficient mixing or distribution is achieved before sample collection.
First Portion Versus Composite Rinse
The concentration of residue in rinse liquid may change during the rinse process.
Early rinse fractions may contain more residue than later fractions. A composite collected across the entire rinse can therefore produce a lower average concentration than an early high-residue fraction.
The sampling strategy should define whether the sample is:
- first portion;
- final portion;
- grab sample;
- composite;
- recirculated homogeneous sample.
The selected approach should correspond to the validation objective. It should not be changed during execution based on which sample produces the preferred result.
Rinse Sample Handling
After collection, the sample should be controlled to preserve the residue concentration until analysis.
The procedure should define:
- sample container;
- fill volume;
- closure;
- labeling;
- temperature;
- protection from light where required;
- maximum hold time;
- mixing before subsampling;
- preservation if scientifically justified.
Residues may adsorb to sample containers, degrade, precipitate, volatilize, or undergo microbial changes during storage.
FDA’s laboratory-controls Q&A specifically notes that holding-time effects should be assessed for TOC samples when storage before analysis can affect accuracy or quantitation capability.
Rinse Blanks and Background
Appropriate blank controls should reflect the analytical method.
Possible controls include:
- incoming rinse-water blank;
- solvent blank;
- container blank;
- process blank;
- sampling-line blank where relevant.
For TOC and conductivity especially, the incoming rinse liquid can contribute measurable background.
Background treatment should be predefined and scientifically justified rather than subtracted retrospectively simply because a result approaches the acceptance criterion.
Combination with Swab Sampling
A strong cleaning-validation strategy often combines:
- Swabs — localized accessible worst-case surfaces.
- Rinse samples — inaccessible or broad internal pathways.
- Visual inspection — whole accessible equipment condition.
This combination provides different forms of evidence rather than three redundant versions of the same test.
Swab Sampling for Cleaning Validation should directly challenge accessible hard-to-clean locations. Rinse sampling should extend coverage to surfaces that cannot be sampled directly.
A passing system rinse should not be used to override a failing worst-case swab.
Validation of the Rinse Sampling Procedure
The rinse sampling method should be demonstrated to be suitable for its intended purpose before it is relied upon for cleaning-validation conclusions.
The supporting evidence should address:
- residue solubility or extractability;
- surface-material compatibility;
- rinse volume;
- contact conditions;
- distribution;
- equipment configuration;
- recovery;
- analytical capability;
- collection;
- sample handling;
- holding time;
- blanks;
- acceptance calculation.
FDA’s historical cleaning-validation inspection guide states that, for an indirect rinse test, firms should establish that the method can distinguish an unacceptable dirty condition rather than simply produce acceptable low results after cleaning.
The practical principle remains valid: a sampling method that cannot respond meaningfully to residue should not be used as evidence that residue is absent.
Protocol Requirements
The cleaning-validation protocol should identify the rinse sampling procedure sufficiently to permit reproducible execution.
It should define or reference:
- equipment represented;
- reason rinse sampling is used;
- surfaces or flow path represented;
- final process rinse versus dedicated analytical rinse;
- rinse solvent;
- volume;
- contact time;
- temperature where relevant;
- flow or recirculation condition;
- equipment configuration;
- valves and routes;
- collection point;
- sample timing;
- recovery factor;
- analytical method;
- acceptance criterion;
- sample handling.
ICH Q7 expects the cleaning-validation protocol to identify the types of samples collected and how those samples are obtained and labeled.
Rinse Sampling Deviations
Rinse-sampling deviations can materially affect the validity of the result.
Examples include:
- incorrect rinse volume;
- wrong solvent;
- incorrect valve configuration;
- incomplete circulation;
- wrong flow path;
- insufficient contact time;
- wrong sample point;
- lost rinse volume;
- incomplete drainage;
- incorrect sample container;
- excessive sample holding time.
An incorrect rinse volume directly changes the concentration calculation. A wrong valve position can exclude a product-contact pathway entirely. The impact should therefore be evaluated technically rather than treating rinse collection as a simple laboratory sampling event.
Unacceptable Rinse Results
A rinse result above the acceptance criterion should trigger investigation of the cleaning process and sampling process.
The investigation should consider:
- residue identity;
- cleaning execution;
- equipment configuration;
- dirty hold time;
- rinse flow path;
- recovery;
- sample collection;
- rinse volume;
- analytical validity;
- prior results;
- associated swab and visual findings.
A repeated rinse should not automatically replace the original result because the first rinse may have removed much of the residual material. Any resampling strategy should therefore be scientifically justified through Cleaning Validation Deviations, Failures, and Investigations.
Routine Verification
After cleaning validation, rinse sampling can be used as part of a risk-based routine residue-monitoring program when supported by validation evidence.
FDA recommends a risk-based post-validation monitoring strategy to demonstrate continued cleaning performance. Routine use may be particularly practical for closed CIP systems where sampling a defined final rinse can be integrated into normal operations.
The routine method should remain consistent with the validated configuration, volume, collection point, analytical method, and acceptance basis.
Lifecycle Control
The rinse method should be reassessed when changes affect the surfaces represented, extraction efficiency, dilution, or analytical interpretation.
Potential triggers include:
- equipment modification;
- new valve or piping configuration;
- new hose;
- different product-contact material;
- revised rinse volume;
- new solvent;
- changed CIP recipe;
- new product or residue;
- different analytical method;
- changed recovery;
- revised residue limit;
- changed sample point.
A small engineering change can alter which surfaces are contacted by the rinse. A new product may have much poorer solubility in the existing rinse solvent. An increased rinse volume may lower the resulting concentration below the analytical LOQ.
These impacts should be assessed prospectively through change control.
Common Rinse-Sampling Deficiencies
A common deficiency is relying exclusively on rinse samples even though accessible worst-case surfaces could be sampled directly. FDA explicitly identifies this limitation.
Other deficiencies include:
- treating incoming-water quality as proof of residue removal;
- failing to demonstrate residue solubility in the rinse liquid;
- uncontrolled rinse volume;
- undefined contact time;
- undocumented valve configuration;
- assuming that all product-contact surfaces receive equivalent rinse coverage;
- failing to demonstrate recovery;
- excessive dilution;
- analytical LOQ above the rinse criterion;
- converting bulk rinse concentration into a local µg/cm² claim without qualification;
- ignoring localized residue because the system-average result passes.
Additional weaknesses include treating a dedicated analytical rinse as an undocumented cleaning step, repeating rinse sampling after an unacceptable result without considering that the first rinse removed residue, and changing the sample location or rinse volume during validation.
Key Principles
- Rinse sampling is an indirect cleaning-validation method particularly suited to inaccessible product-contact surfaces and closed equipment pathways.
- A final process rinse and a dedicated analytical rinse are different sampling concepts and should be defined separately. The former evaluates liquid generated by the approved cleaning procedure; the latter is a controlled post-cleaning extraction performed specifically for analytical verification.
- Rinse-liquid selection should be based on demonstrated recovery of the residue of concern and compatibility with the equipment and analytical method.
- Rinse volume, contact time, hydraulic distribution, valve configuration, system route, drainage, and sample collection point determine which surfaces the rinse result can legitimately represent.
- A rinse result is an averaged system-level measurement. Localized residue can be diluted into a large liquid volume, and a passing rinse result therefore does not demonstrate that every individual product-contact surface is below a corresponding local surface criterion.
- Rinse sampling should normally complement direct surface sampling where accessible worst-case locations can be swabbed. FDA specifically states that rinse-only validation is generally inadequate when direct surface measurement is feasible.
- Recovery, analytical sensitivity, sample handling, blanks, and holding time should be demonstrated for the complete rinse method.
- The rinse sampling procedure should remain under lifecycle control as products, equipment configuration, cleaning procedures, rinse conditions, analytical methods, and residue limits change.